
 AS/RS Handling Robot
 Vertical Storage Module
 Conveying Equipment
 Smart Warehousing System
 Warehouse Racking
 Industries
 Services
 About Us
High-Quality Chain Conveyors from Trusted Suppliers and Factories
When it comes to efficient materials handling, our Chain Conveyor systems stand out in the industry. As a buyer, you deserve to work with high-quality suppliers who understand the unique demands of your operations. That's why we offer advanced Chain Conveyor solutions tailored to meet your specific needs, Our products are designed and manufactured with precision, ensuring they can handle even the most challenging environments. Whether you're in food processing, packaging, or any other sector, our Chain Conveyors offer reliability and durability that you can trust

Champions of Chain Conveyor Factory Application
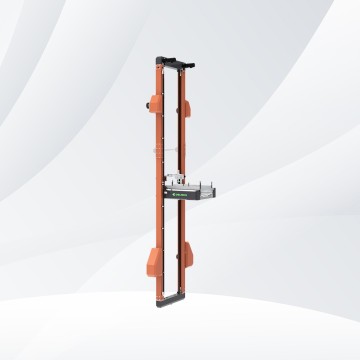
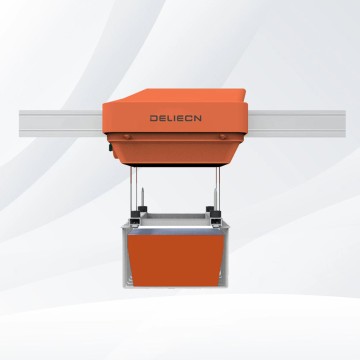
In today's fast-paced manufacturing environment, the efficiency of material handling systems plays a pivotal role in determining operational success. Chain conveyors have emerged as champions in various applications, enabling businesses to streamline logistics and improve productivity. Their robust design and versatility allow for the seamless movement of goods across different production phases, making them ideal for industries ranging from food and beverage to automotive. The adoption of automated chain conveyor systems is transforming intralogistics by integrating cutting-edge robotics technologies that enhance not only speed but also accuracy in material transportation. These automated systems can be tailored to meet specific operational requirements, supporting modular setups that adapt as businesses evolve. Additionally, effective inventory management is crucial for maximizing warehouse space, and chain conveyors can significantly reduce manual handling, alleviating bottlenecks and ensuring smoother workflows. Investing in advanced chain conveyor solutions provides businesses with the opportunity to stay ahead in a competitive landscape. By leveraging end-to-end automation, companies can optimize their supply chain processes, reduce operational costs, and improve overall efficiency. As global demand for innovative logistics solutions continues to grow, the implementation of reliable chain conveyors will be key to achieving sustainable operational excellence.
Champions of Chain Conveyor Factory Application
| Application Area | Conveyor Type | Load Capacity (kg) | Speed (m/s) | Material Type | Environment |
|---|---|---|---|---|---|
| Automotive Assembly | Roller Chain Conveyor | 500 | 1.5 | Steel | Indoor |
| Food Processing | Modular Plastic Chain Conveyor | 300 | 1.2 | Plastic | Humid |
| Packaging | Heavy-Duty Chain Conveyor | 1000 | 1.0 | Steel | Indoor |
| Material Handling | Slat Chain Conveyor | 1.3 | Plastic | Outdoor |
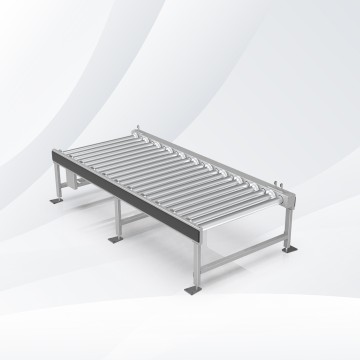
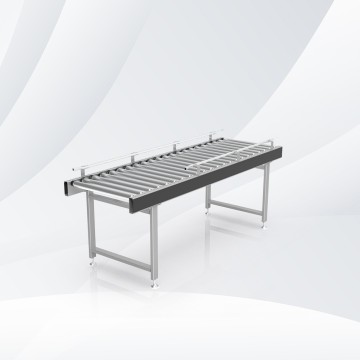
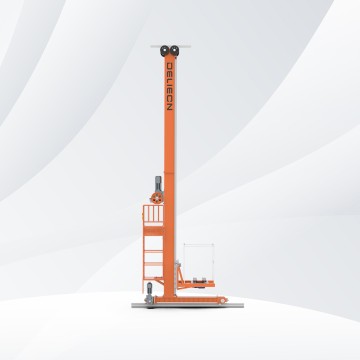
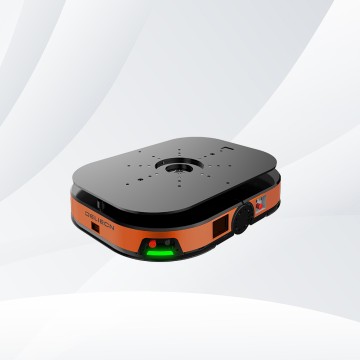
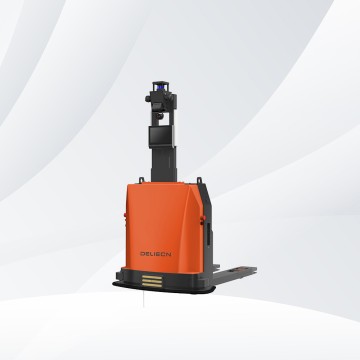
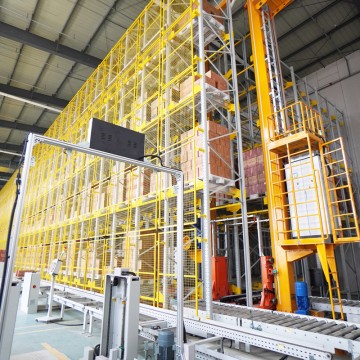
Trending Chain Conveyor Trusted by Pros Guarantees Peak Performance
H
Hannah Roberts
The product quality is top-notch. The service team handled my inquiries efficiently.
13 May 2025
S
Sadie Ramirez
I couldn’t be happier with my choice! The support team was informative and courteous.
21 May 2025
L
Lillian Cox
Highly impressed with the product! The staff response time was excellent.
22 May 2025
S
Sophie Rivera
Quality is outstanding! The support I received was timely and exceptionally helpful.
13 May 2025
Z
Zachary Sanders
Great value for the money! The support team was efficient and friendly.
25 May 2025
S
Sadie Bailey
The quality is unparalleled! Their team made sure I felt supported throughout.
09 May 2025