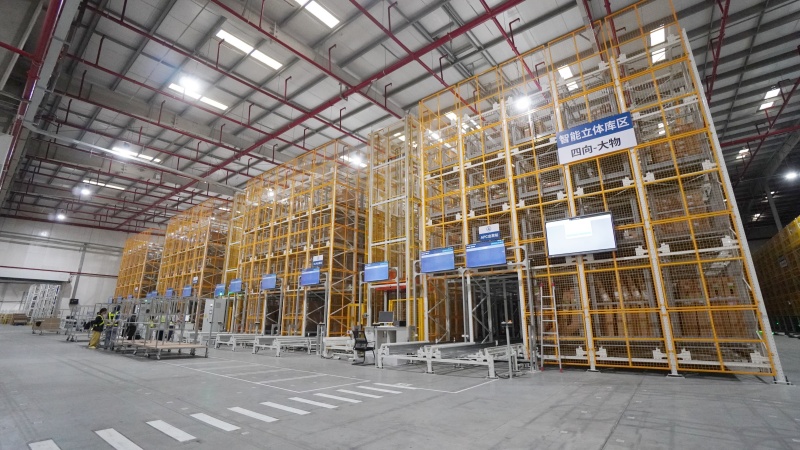
Most Pallet Shuttle suppliers can tell you how fast their robot travels, how much weight it carries, and how many pallets fit into a rack.
Those figures are useful, but they rarely explain why one supplier can handle a complex warehouse project and another struggles once commissioning begins.
The difference usually appears in the questions they ask before proposing a system.
An automotive spare-parts warehouse does not operate like a pharmaceutical factory. A chemical plant running around the clock has very different priorities from a cold store. Even two warehouses using the same Pallet Four-Way Shuttle Robot may need different rack layouts, transfer methods, WMS/WCS logic, and redundancy strategies.
This is why I would not judge a Pallet Shuttle System supplier by the robot alone.
A better place to start is the supplier's understanding of the industry in which the robot will actually work.
Automotive Projects Quickly Expose Whether a Supplier Understands the Load
Automotive spare-parts storage sounds like a standard pallet application until the actual inventory is reviewed.
At Toyota's spare-parts center, the warehouse manages nearly 45,000 SKUs across several operating areas. Large parts are stored in steel cages, and the cages do not all have the same height.
That seemingly small detail affected the storage design.
The first rack level was planned for cages up to 1,675 mm, while the upper four levels were designed around cages up to 1,200 mm. If the tallest cage specification had simply been applied to every level, a large amount of vertical space would have been wasted.
The Pallet Shuttle area eventually provided approximately3,091 pallet and cage positions, using 14 Pallet Four-Way Shuttle Robots and four Lifters.
This is the kind of case I would ask a potential supplier about.
Not “Have you worked in automotive?”
Ask instead:
How did the load carrier affect the rack design?
How were different cage heights handled?
How were the shuttle quantity and lifter capacity determined?
If the answer never goes beyond robot speed and storage density, the supplier may understand the equipment without fully understanding the application.
Pharmaceutical Warehouses Change the Conversation Again
A pharmaceutical customer usually raises different concerns.
The warehouse may be storing packaging materials, finished products, pharmaceutical raw materials, and processed materials at the same time. The system has to know where each pallet is, what material it contains, and how that movement relates to production or shipping.
At a pharmaceutical project in ZhengLai, Pallet Four-Way Shuttle Robots were used as part of the automated warehousing process for packaging materials and finished goods.
The the finished-goods warehouse provided 893 pallet locations. Operational accuracy reached 99.9%, and the automated logistics process helped reduce labor input by approximately 60%.
The important part was not simply creating more pallet positions.
WMS recorded inventory changes and material movements so that finished goods, raw materials, and packaging materials could be traced through the warehouse process.
A supplier experienced in pharmaceutical logistics should naturally start asking about material zoning, batch information, FIFO rules, production supply, traceability, and upstream system interfaces.
If the first discussion is still dominated by “maximum speed” and “maximum load,” something important is missing.
Chemical Warehouses Put More Pressure on the Whole System
Chemical projects reveal another side of supplier capability.
In a magnesium sulfate project, the warehouse had to receive several finished-product formats from continuous production, including 50 kg woven bags and 1-ton bulk bags.
The system was designed with 6,309 pallet positions, 13 Pallet Four-Way Shuttle Robots, and four Lifters.
But those numbers only tell part of the story.
The real design question was how to connect packaging, inbound inspection, high-density storage, level changing, outbound handling, and loading without creating a bottleneck somewhere in between.
One decision was to use fork-type pallet lifters rather than installing conveyor transfer stations throughout all 13 storage levels. This reduced the amount of motors, chains, sensors, and other equipment installed inside the high-bay rack.
That mattered both for the initial investment and for later maintenance.
The shuttle itself also used mechanical lifting rather than hydraulic lifting, avoiding hydraulic-oil leakage risk in a powder chemical environment.
These are not headline specifications. They are details that appear when a supplier has actually spent time solving chemical warehouse problems.
A Good Proposal Should Look Different From Project to Project
This is probably the easiest way to judge whether a supplier has real application experience.
Give the same supplier an automotive project, a pharmaceutical project, and a chemical project.
The proposals should not look like the same warehouse with different dimensions.
Toyota's design had to respond to different cage heights and a large, mixed spare-parts operation.
The ZhengLai pharmaceutical project had to connect pallet storage with material management and traceability.
The magnesium sulfate project had to accommodate continuous production, heavy finished goods, powder-environment considerations, and different outbound processes.
The shuttle technology can come from the same product platform. The engineering around it should change.
That is where industry insight begins to show.
WCS Matters More as the System Gets Larger
Another useful way to compare suppliers is to move the discussion away from one robot and ask what happens when many robots are working.
In one battery-material warehouse, more than 30 Pallet Four-Way Shuttle Robots operate in a facility with nearly 40,000 pallet positions and pallets weighing more than one ton.
At that scale, adding another robot does not automatically increase throughput.
WCS has to consider where each shuttle is, which task is urgent, whether a lifter is available, and where congestion may develop. If one robot becomes unavailable, unfinished work should be redistributed where the system layout allows it.
This is why software capability should be evaluated with the hardware.
A supplier should be able to explain how the system behaves when several tasks arrive together, not just demonstrate one shuttle completing one movement.
Pay Attention to Who Actually Builds the System
Pallet shuttle projects usually involve more than shuttle robots.
There are racks, Lifters, conveyors, WMS/WCS, interfaces with ERP or MES, electrical control, installation, and commissioning.
When these parts come from many unrelated suppliers, project responsibility can become unclear during commissioning.
DELIECN develops and manufactures approximately 90% of its core hardware and software in-house.
For a customer, the relevant point is not the percentage itself. It is whether the people responsible for the shuttle, the WCS, and the transfer equipment can solve an interface problem together when the site does not behave exactly as predicted.
That is worth asking every supplier:
Which parts of the proposed system are yours, and who takes responsibility when two systems do not work together as expected?
The Best Supplier Is Usually the One That Understands the Warehouse Before Selling the Robot
There is no single pallet shuttle supplier that is automatically best for automotive, pharmaceutical, chemical, cold-chain, and manufacturing projects.
The better supplier is the one that recognizes those differences early enough to change the design.
When comparing suppliers in 2026, look at their completed projects and ask what was difficult about them. Ask what changed between the first proposal and the final implementation. Ask how the system handles peak periods, maintenance, expansion, and software interfaces.
Then compare the robot specifications and price.
A Pallet Shuttle Robot is an important part of an AS/RS, but it is only one part.
What customers finally live with for the next several years is the whole warehouse system—and the engineering decisions behind it.
FAQS
: Check industry experience, completed projects, WMS/WCS capability, system integration, scalability, and after-sales support.
Automotive, pharmaceutical, chemical, and cold-chain warehouses have different storage, safety, and traceability requirements. Relevant experience helps avoid design mistakes.
Two-way shuttles suit deep-lane storage, while four-way shuttles offer more flexibility for cross-lane and multi-level operations.
WMS manages inventory and business rules; WCS coordinates shuttle robots, Lifters, conveyors, and task execution.
Ask for comparable cases with real data such as pallet locations, throughput, load weight, shuttle quantity, and operating conditions.

 Industries
 Services
 About Us
 AS/RS Handling Robot
 Vertical Storage Module
 Conveying Equipment
 Smart Warehousing System
 Warehouse Racking